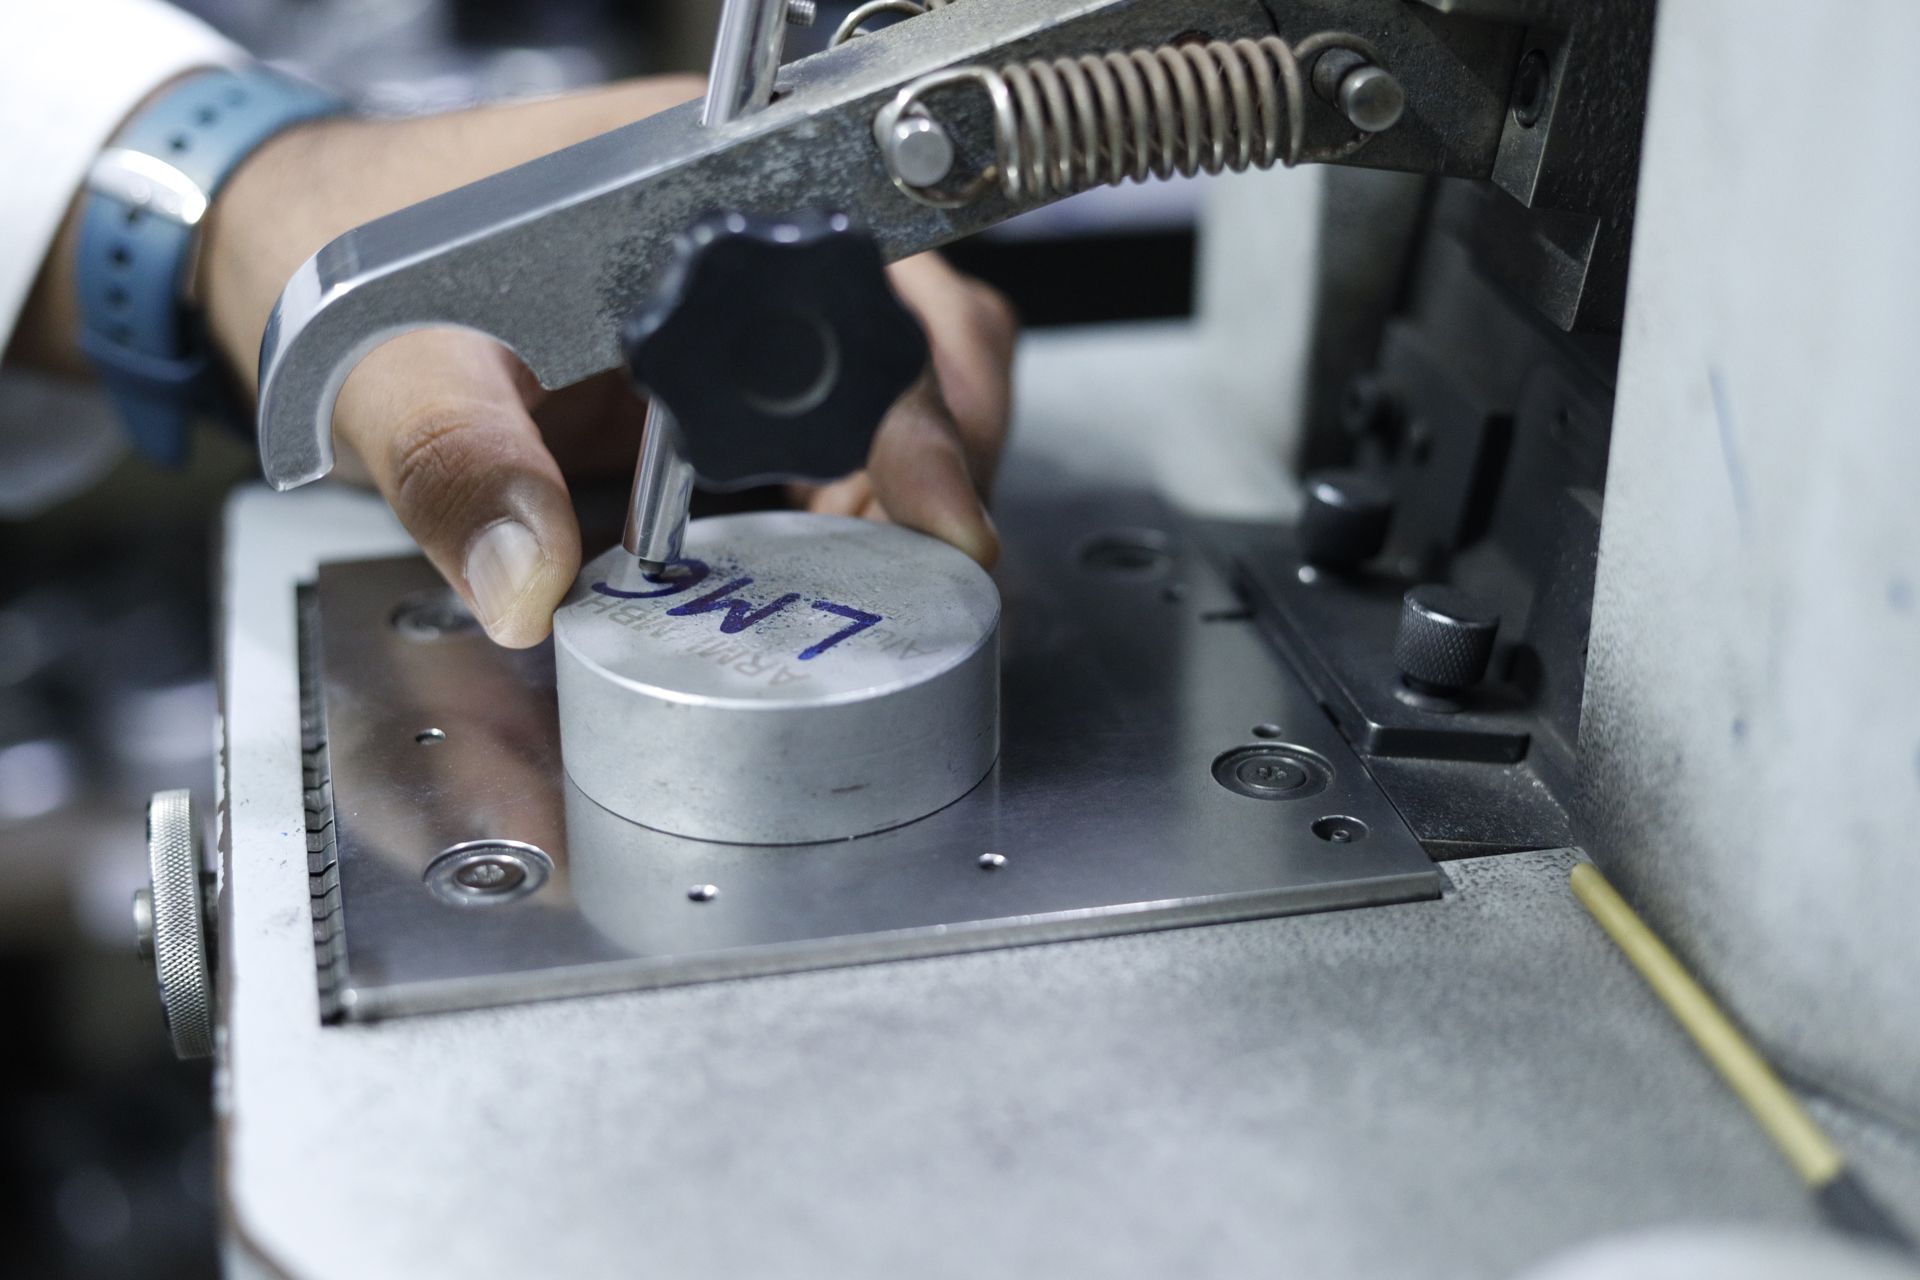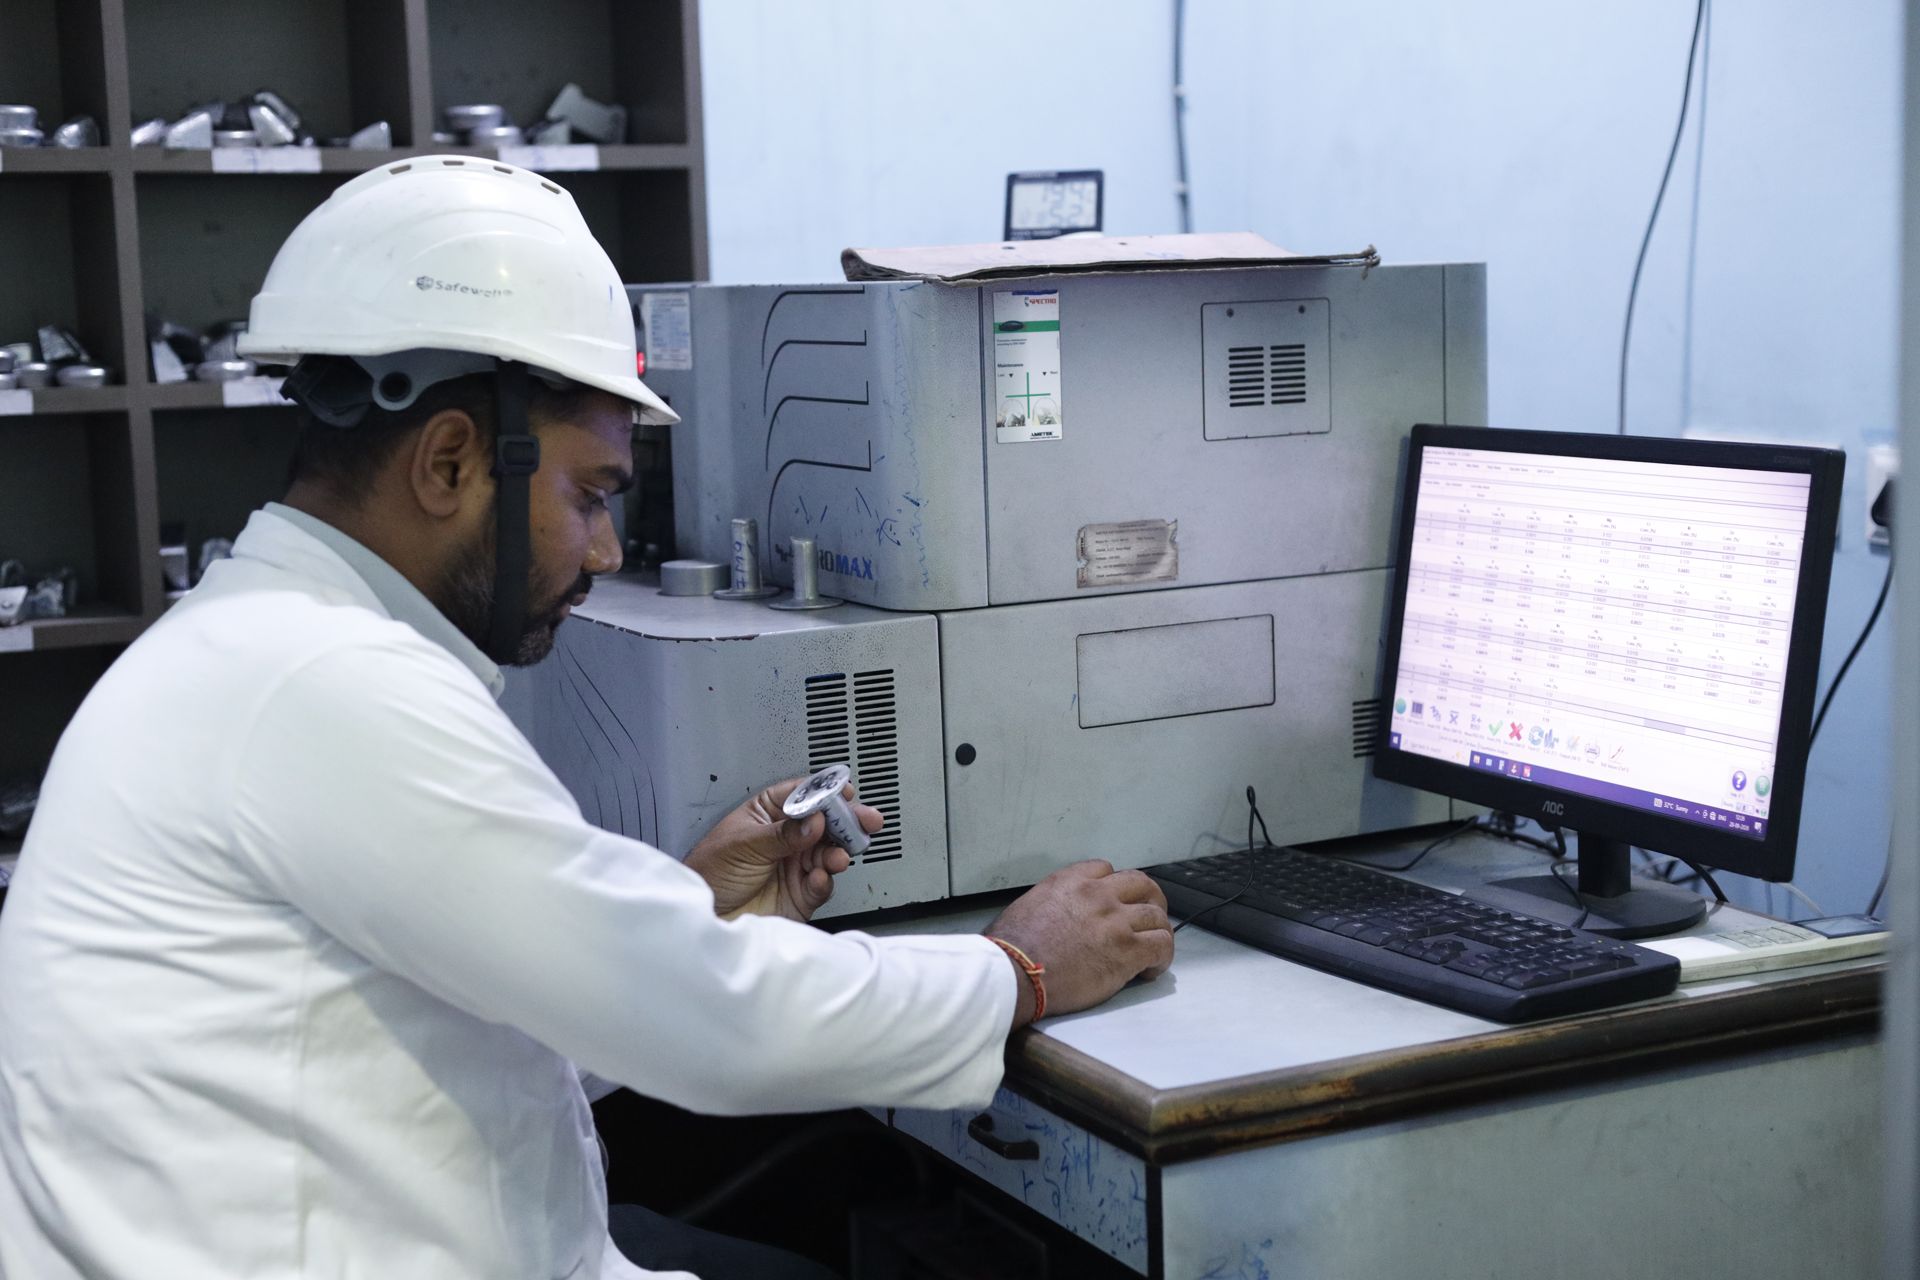
Equipped with high-efficiency Skelner & Crucible furnaces, Optical Emission Spectrometers, and heavy material handling fleets.
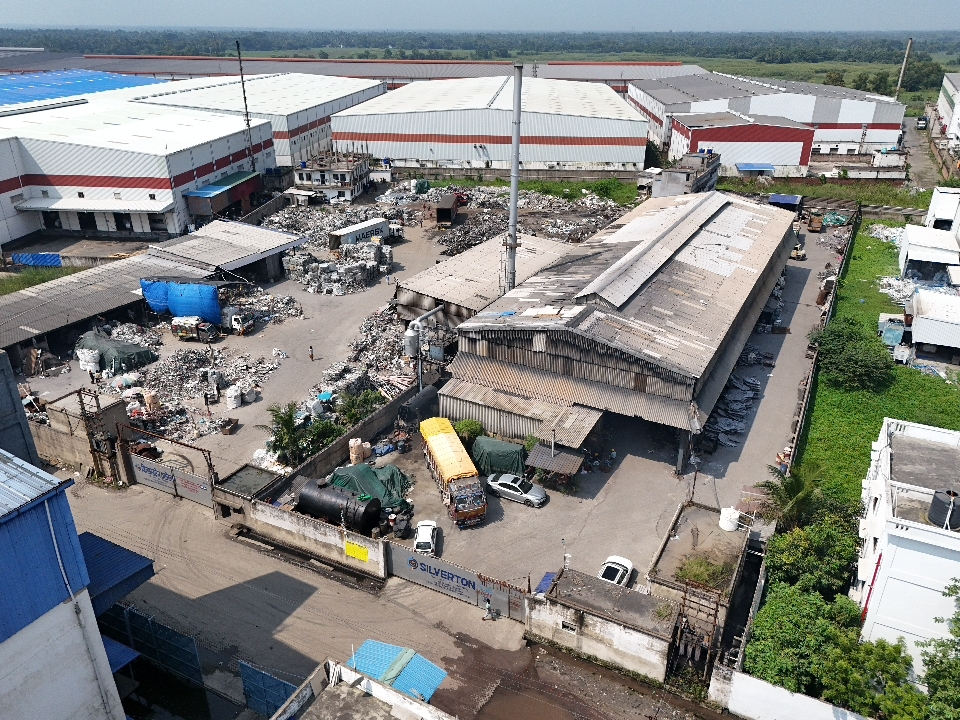
Sri Ram Hanuman Complex, Ranihati, Amta Road, Howrah – 711322
GSTIN: 19AADCS8376B1Z5
Our flagship Howrah facility features eco-friendly Skelner and crucible furnaces and automatic ingot casting lines for tailor-made wheel and piston alloys.
S.F.No. 176/2, 3, Suluk Taluk, Pappampatti Village, Chinnakuyili Petrol Bunk Cut Road, Coimbatore – 641016
GSTIN: 33AADCS8376B1ZF
Strategic Southern manufacturing hub catering to automotive and electrical component foundries across South India with rapid delivery cycles and ISO 14001 / ISO 45001 EMS safety accreditations.
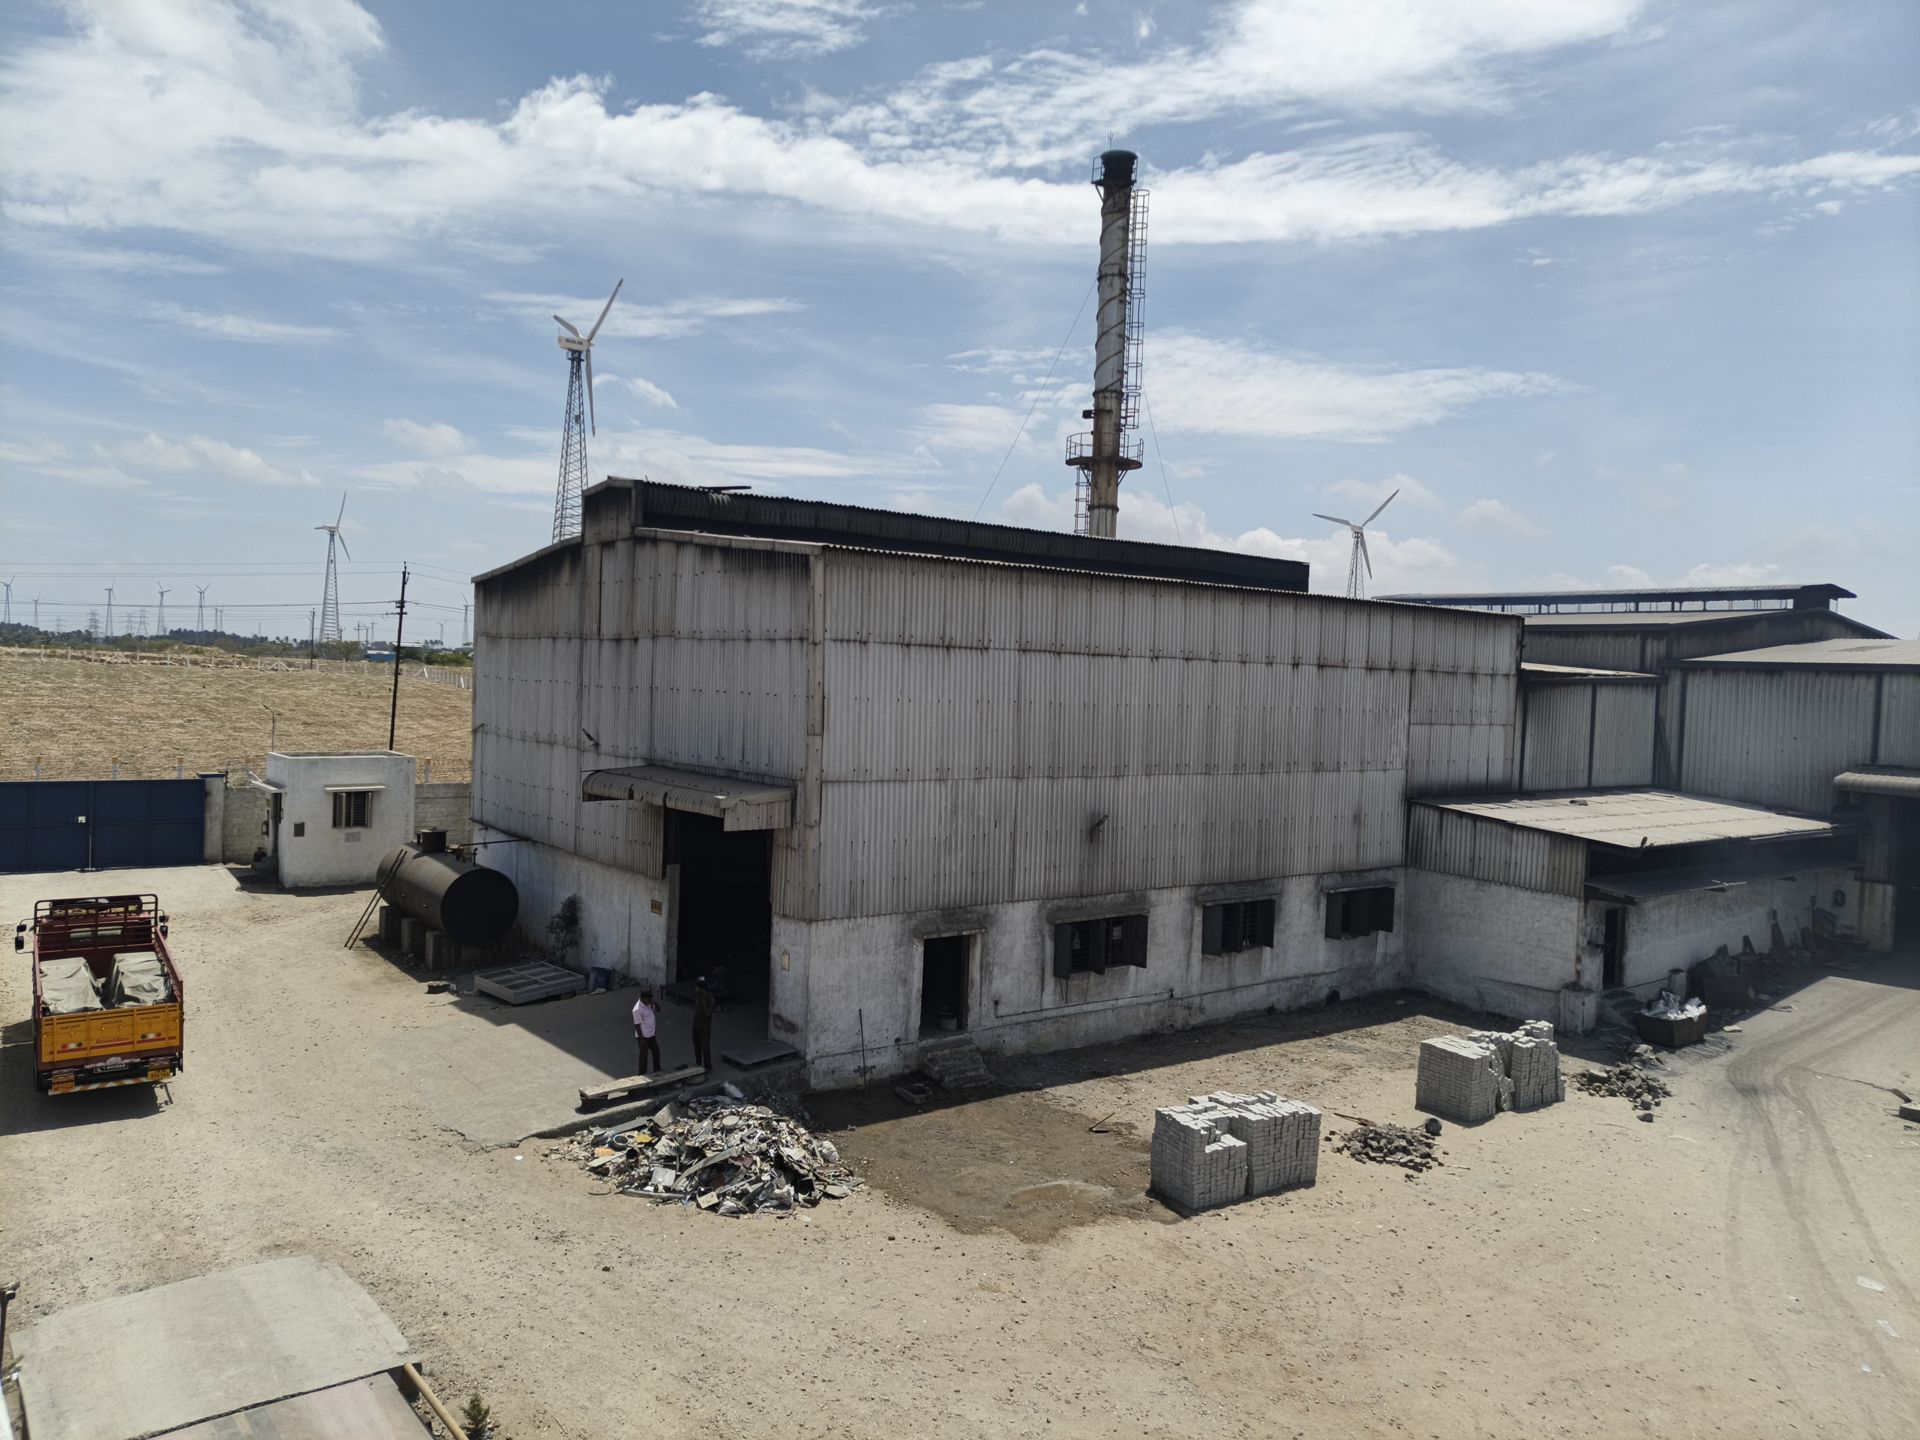
Advanced furnaces, spectro-analysers, dross recovery systems, and material handling fleet across our units.
2 in Plant 1, 1 in Plant 2
4 in Plant 1, 2 in Plant 2
2 in Plant 1, 1 in Plant 2
1 Hot Dross Processing Machine in each Plant
Plant 1
Ball Mill Machine, Pulverizer, Magnetic Separator - 1 Unit in each plant
Electric Furnace, Band Saw Machine, Abrasive Belt Grinding Machine - Plant 1
3 in Plant 1, 1 in Plant 2
1 in Plant 1
Comprehensive 19-step quality assurance workflow from raw material purchasing to final delivery.
All scraps are purchased by our experts after thorough assessment
Our group of expert sorters segregate the lot manually and remove all non metallic/non aluminium material to create a homogeneous batch of scrap
Random sampling of the segregated RM is done for quality control
Our production team selects and forms a batch mix of different types of scraps suitable for a particular grade
The selected batch is then transferred into our furnaces
After the material is melted, all the ash and residue is scooped out of the furnace
A sample of the molten metal is tested in our lab in the Spectro meter
After sampling, our production manager selects further raw material for alloying and correction
Again the ash and residue is scooped out of the furnace
Nitrogen/Argon degassing along with other treatment is done for removing porosity and grain refinement
Another sample is drawn from the batch and tested to check whether the metal is in the range of the particular grade. If not, corrective raw material is further charged
After the Lab incharge approves the final sample, the molten metal is casted in our moulds
While pouring, any residue on the surface of the mould is scooped out
While the molten metal is semi hard, batch no and grade is embossed on the ingot
After pouring is completed, all the ingots are stacked in piles
The piles are then labelled and colour coded according to the customers specifications
Random samples of ingots are selected from the piles and tested again for quality control
The piles are then packed for delivery
All the piles are loaded in vehicles and released for delivery.